A quote for cartridge filling machines can look complete while hiding five unresolved decisions: how material leaves the bulk container, how the dose is measured, how the cartridge moves during filling, how the package closes, and what evidence releases the machine. A buyer who compares only output speed is comparing incomplete systems.
Key Takeaways
- Freeze the adhesive, source container, cartridge, piston, cap, label, and finished-package checks before requesting a machine.
- Treat bulk unloading, material conditioning, metering, filling, closing, marking, and inspection as one connected architecture.
- Select automation against sustained released output, changeover work, and operator ownership—not a headline cycle rate.
- Keep single-component and dual-component requirements separate until the supplier proves the relevant material paths and package interfaces.
- Use the actual adhesive and production package during acceptance; water or an easy surrogate cannot expose the same feed, cutoff, or closure risks.
- Haijing documents at least 72 hours of functional and stability testing before filling equipment ships, but the agreed test scope still belongs in the purchase contract.
The strongest request for quotation describes the operating envelope and the proof required at factory acceptance. This guide shows how to build that request without borrowing another plant’s unverified accuracy, viscosity, or rate claims.
Start With The Filled Package
Machine selection starts at the finished package, not at the pump. Name the cartridge family, capacity, chamber ratio, outlet, piston or rear closure, front cap, label, batch mark, and pack-out. Then identify the adhesive formulation class and source container. If any of these fields are open, a supplier must quote assumptions instead of an engineered boundary.
A drawing is more useful than a photograph. It defines the body and closure interfaces that the machine must locate, support, fill, and close. Link the drawing to the approved component kit described in the empty silicone and adhesive cartridge guide. The available adhesive cartridge systems establish the package families that the equipment study must narrow. A later change to piston geometry or outlet closure can alter the machine fixture and acceptance plan even when the nominal capacity stays unchanged.
| Package Field | Machine Consequence | Release Evidence |
|---|---|---|
| Cartridge body | Fixture, orientation, fill stroke | Controlled drawing and samples |
| Piston or closure | Insertion tool and seating motion | Position and seal check |
| Front outlet and cap | Pre-fill closure and leak boundary | Approved component set |
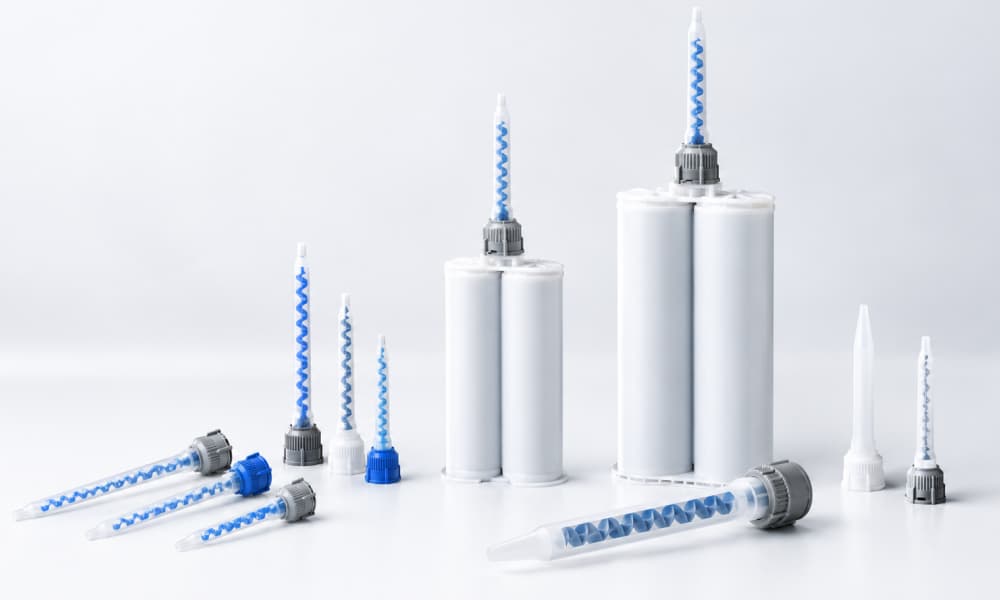
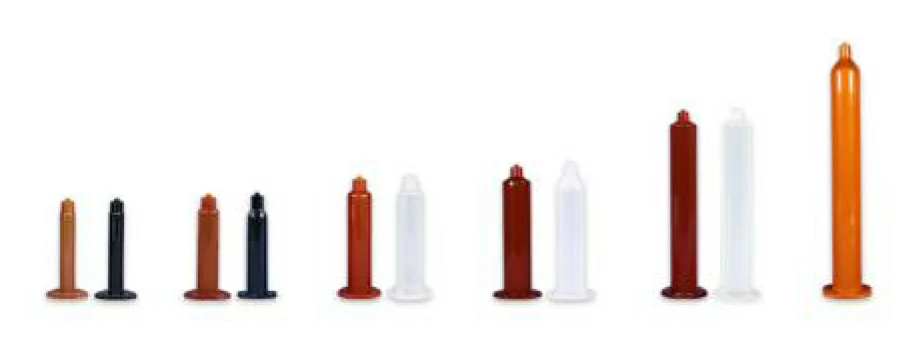
Do not collapse every package into “a cartridge.” Haijing‘s documented single-component range includes 100, 200, 300, 310, 400, 500, 1000, and 2600 ml formats. Its documented dual-component range runs from 50 through 1500 ml in 1:1, 2:1, 4:1, and 10:1 configurations. Those are package families, not a claim that one filling machine covers every format.
Map The Complete Machine Architecture
A cartridge filler is rarely one isolated station. The working system begins where bulk material enters the process and ends where a traceable closed package leaves it. Between those points sit material supply, conditioning if required, a metering device, the fill valve and motion, cartridge handling, closure insertion, marking, inspection, rejection, and pack-out.
The boundary matters because each handoff can defeat the station beside it. A stable meter cannot rescue an interrupted supply. Clean bottom-up motion cannot correct an incompatible piston tool. A fast filler can build a queue if closure insertion or labeling remains manual. Put every function on one process map and name the party who owns it.
| Subsystem | Decision To Freeze | Hidden Handoff Risk |
|---|---|---|
| Bulk supply | Source container and change method | Starved or interrupted feed |
| Material path | Wetted parts and conditioning | Reaction, abrasion, or heat exposure |
| Metering | Dose basis and verification | Unclear accuracy claim |
| Fill motion | Nozzle and cartridge movement | Air or inconsistent cutoff |
| Closing | Closure identity and seating | Trapped air or damaged package |
| Inspection | Checks, limits, and reject path | Defects mixed with released output |
Procurement warning: if two quotes use different system boundaries, their prices and rates are not comparable. Ask each supplier to mark included equipment, buyer-supplied equipment, utilities, interfaces, and excluded end-of-line work on the same process map.
Choose The Right Automation Level
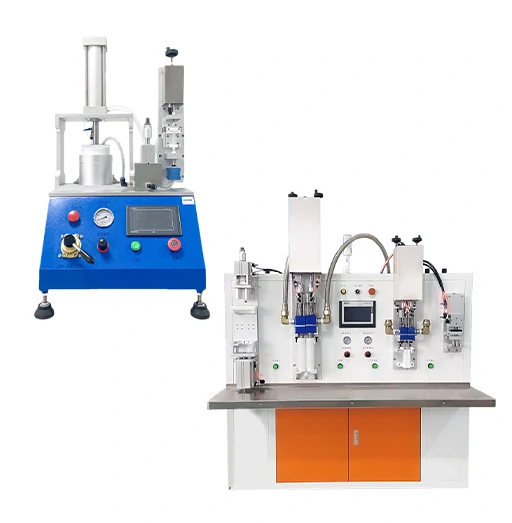
Manual, semi-automatic, and automatic lines solve different operating problems. A bench or manual line gives the operator control of cartridge loading, fill initiation, closing, and pack-out. It is a defensible choice for varied formats or lower demand when trained labor and clear work instructions are available. Its real constraint is repeatability across operator actions and transitions.
A semi-automatic cell automates the dose or fill cycle while leaving cartridge presentation, closure, or transfer to an operator. This architecture can reduce capital and simplify changeover, but only if the person can sustain the required loading and unloading sequence. Ergonomics, material replenishment, and queue control belong in the cycle study.
An automatic line connects handling, filling, closing, marking, inspection, and reject control. Nannini Renato publishes model-dependent examples from 25 to more than 80 cartridges per minute for single-, double-, and triple-head systems. That vendor example proves the range of available architectures; it does not set a rate for your adhesive or package.
Choose the lowest automation level that meets the released-output requirement with a controlled process. Buying more stations does not remove process ownership. It adds interfaces, sensors, recipes, guarding, spare parts, and change-control work that the plant must support.
Match The Feed System To Material
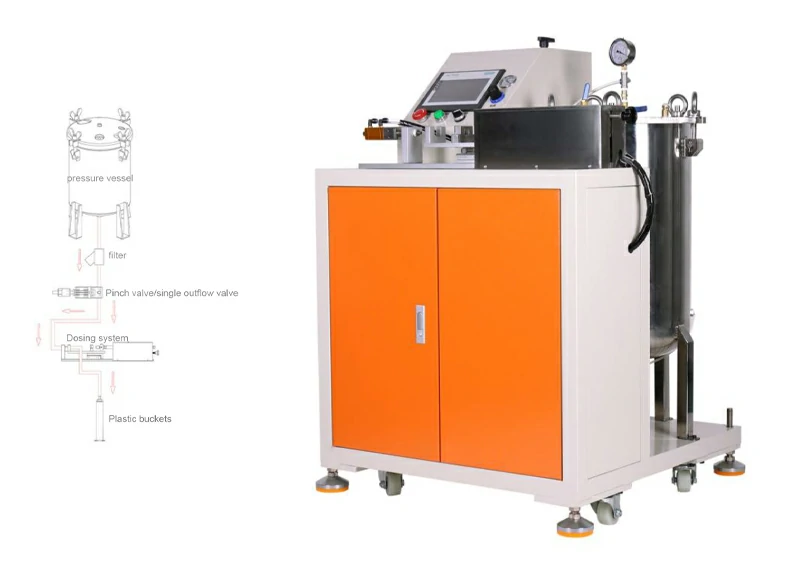
Start the material path with the incoming container. Nannini Renato documents systems that unload 20–25 liter pails, 200 liter drums, or production tanks before feeding the doser. Graco describes supply systems that transfer medium- to high-viscosity one-component sealants and adhesives from pails or drums to metering and dispensing equipment. Both sources make the same design point: bulk unloading is part of filling, not an accessory selected later.
Give the supplier the adhesive technical data and safety data, then identify conditions the material path must tolerate. ViscoTec lists viscosity, abrasiveness, solids, shear sensitivity, process temperature, and seal or elastomer selection as relevant inputs. Do not convert those inputs into a generic pump rule. Ask the supplier to show why the proposed wetted path matches the named formulation and cleaning method.
Define Normal And Transition States
A feed system must work during more than steady production. Describe initial prime, normal run, bulk-container change, planned stop, restart, end-of-batch, cleaning, and material change. These states expose starvation, retained material, uncontrolled discharge, and cross-batch mixing that a short steady demonstration can hide.
Make Maintenance Visible
Require a wetted-path drawing, seal list, wear-part list, cleaning access plan, and safe pressure-relief method. The maintenance team should review them before purchase. If a pump or valve can be reached only after removing guarded assemblies, the promised changeover can collapse on the factory floor.
Specify Metering And Fill Motion
“Accurate filling” is not a test method. The RFQ must state what quantity defines a good fill, how it will be measured, which package and material will be used, and when samples are taken. Net mass, delivered volume, component-specific mass, or another approved measure may be appropriate. The plant and supplier must agree before a tolerance can mean anything.
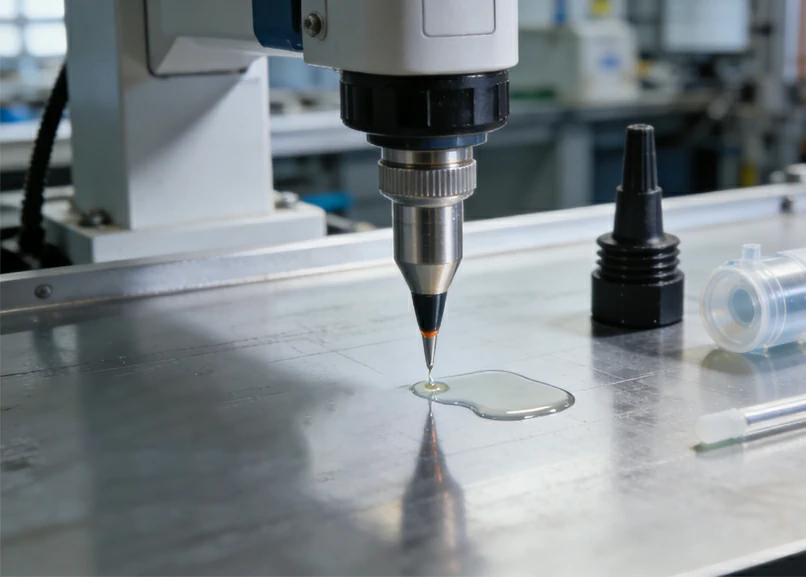
Fill motion also belongs in the specification. Nannini Renato describes vertical filling from the bottom upward with controlled cartridge lowering to reduce bubble formation. The useful lesson is not that one motion guarantees an air-free package. It is that nozzle position, cartridge movement, material delivery, cutoff, and closure form one sequence that must be demonstrated with the actual material.
Challenge Cutoff And Product Tail
Observe the end of every fill. A long tail, drip, smear, or delayed valve response can contaminate the sealing area and shift weight into the next package. Specify the acceptable condition in photographs or retained examples. Words such as “clean” or “minimal” leave too much room for interpretation.
Do Not Hide Air Behind Weight
A package can meet mass while still showing unacceptable voids or closure behavior. Keep dose verification and package-condition inspection as separate gates. The later process guide will cover air control and piston insertion in depth; this machine-selection stage only needs the inspection method, sample locations, and pass/fail ownership frozen.
Freeze The Package Before The Machine
Send the formulation class, source container, cartridge drawing, closure set, output cases, and required acceptance evidence for an engineering review. Haijing can align the package interfaces before the equipment specification is released.
Package drawing | Machine interfaces | Acceptance scope
Separate 1K And 2K Decisions
A single-component line controls one material path and one package dose. A dual-component line must also preserve separation between A and B, address different material behaviors, and verify the result in each chamber. Do not approve a “1K/2K capable” statement without a flow diagram and change-part list for every quoted format.
The cartridge ratio is a geometry relationship, not proof of correct filling. Haijing documents dual-cartridge formats in 1:1, 2:1, 4:1, and 10:1 configurations. The machine acceptance plan should link each approved body drawing to component identity, chamber-specific dose evidence, closure identity, and a method for detecting reversal or cross-connection.
METER MIX documents cartridge and syringe filling from bulk one- and two-part materials with metering and mixing equipment. That application case shows why the architecture must follow the material route. Some projects fill separated components into a dual cartridge; others fill a premixed material into a package. Those are different processes with different cleaning, working-time, and release risks.
Release boundary: the dual-component cartridge specification defines the package. The filling-machine acceptance record must prove that the chosen line fills that specific package without swapping components, damaging the divider, or losing chamber traceability.
Integrate Closing Marking And Inspection
Filling ends only after the package is closed and traceable. Nannini Renato’s line descriptions include capping and ink-jet marking for batch or expiration information. ProSys also presents cartridge systems with vertical bottom-up filling and closure options. Both examples support one practical conclusion: the closure station belongs inside the machine study.
Specify closure identity, orientation, insertion method, seating condition, damaged-part handling, and the check that confirms presence. Then freeze the marking content, location, readability, and recipe link. A correct dose in an untraceable package is not released production.
Give Every Reject A Destination
Define what happens after a failed weight, missing closure, unreadable code, or sensor fault. The machine should prevent a failed unit from rejoining good output without documented disposition. Challenge the reject path during acceptance instead of only proving the pass path.
Count Released Output
Production capacity should count closed, marked, inspected, and accepted cartridges. It should not count empty indexing cycles or filled bodies waiting for manual closure. This definition makes manual, semi-automatic, and automatic proposals comparable on the output the business can actually ship.
Write A Machine RFQ That Works
A useful RFQ lets every supplier answer the same problem. Attach the material documents, package drawings, component samples, process map, output cases, inspection rules, utilities, layout boundary, and destination requirements. Ask suppliers to list exceptions beside each requirement. A polished proposal without an exception register is difficult to compare and harder to enforce.
| RFQ Block | Required Input | Supplier Response |
|---|---|---|
| Material | Named formulations and source containers | Proposed path, limits, exclusions |
| Package | Drawings, closures, labels, samples | Tooling and change parts |
| Production | Normal, peak, changeover, restart cases | Released output and staffing |
| Quality | Measurements and reject rules | Inspection method and records |
| Facility | Layout, utilities, environment | Loads, connections, guarding |
| Lifecycle | Cleaning, maintenance, future formats | Manuals, spares, support plan |
Define the deliverables that make the machine maintainable: layout and interface drawings, electrical and pneumatic documentation, bill of materials, recommended spares, software or recipe backup, operating instructions, maintenance instructions, training, and acceptance records. The exact list should follow the purchased configuration and local obligations.
Write Changeover As A Test Case
Do not ask only for “quick changeover.” Name the start format, end format, parts changed, cleaning state, responsible operator, required tools, and first acceptable output. The supplier can then demonstrate a real sequence. Procurement can compare evidence instead of adjectives.
Run A Testable Factory Acceptance
The factory acceptance test, or FAT, should verify the purchased configuration against agreed requirements before shipment. Haijing documents at least 72 hours of functional and stability testing for filling equipment before delivery. That duration becomes useful only when the protocol names the materials, formats, operating states, observations, sample plan, acceptance criteria, deviations, and approvers.
Use the real adhesive whenever it can be handled safely and legally at the supplier site. If a substitute is unavoidable, document which properties it represents and which risks remain open for site acceptance. Never let a surrogate trial silently become proof of compatibility with the production formulation.
| FAT State | What To Challenge | Evidence To Retain |
|---|---|---|
| Startup | Prime, first fills, first closures | Sequence, samples, observations |
| Normal run | Feed, dose, motion, close, inspect | Raw results and accepted units |
| Bulk change | Interruption and return to control | Time-stamped transition record |
| Format change | Parts, recipe, setup, first-off | Change list and approval |
| Planned stop | Hold condition and restart | Restart samples and disposition |
| Fault and reject | Alarm, safe state, segregation | Fault log and reject proof |
Record failures without tuning them out of the history. If the supplier changes a valve setting, fixture, recipe, or sensor threshold, capture the old state, reason, new state, and repeated test. This follows the same evidence principle used in the 2K cartridge supplier-claim guide: preserve the failing condition before corrective action destroys the evidence.
Close The Punch List Deliberately
Classify every open item by release impact, owner, evidence required, and due point. A cosmetic label issue does not carry the same risk as an unverified reject path or unstable material feed. The contract should state which items block shipment and which can move to site acceptance.
Use A Decision Matrix Before Purchase
Score fit before price. Begin with knockout criteria: material compatibility, package coverage, component separation where required, safe operation, agreed inspection, and a testable acceptance plan. A proposal that fails a knockout condition should not win through a high score elsewhere.
Then compare system boundary, released output, changeover burden, operator work, maintainability, documentation, spare parts, support, and future-format ownership. Use the same evidence request for every supplier. If one score rests on a brochure adjective and another rests on a witnessed trial, they are not equal inputs.
| Decision Area | Strong Evidence | Weak Evidence |
|---|---|---|
| Material path | Reviewed wetted-path design | Generic compatibility claim |
| Package coverage | Drawing-linked tooling list | Similar cartridge photo |
| Output | Accepted units in defined run | Unqualified cycle rate |
| Changeover | Witnessed transition and first-off | “Fast” or “tool-free” |
| Quality | Raw measurements and reject proof | Pass statement only |
| Lifecycle | Manuals, spares, backup, training | Support available on request |
The best cartridge filling machine is the one that can be released, operated, changed, maintained, and investigated within the buyer’s real factory. That conclusion may favor a simpler cell over a larger automatic line. It is still the stronger engineering decision.
References
- Nannini Renato automatic cartridge filling lines — bulk supply, bottom-up filling, closing, marking, and vendor-specific line configurations.
- METER MIX cartridge filling application — metering and filling one- and two-part materials from bulk supply.
- ViscoTec filling systems — material and process inputs for pump and seal selection.
- ProSys cartridge filling machines — vertical filling architectures and closure options.
Frequently Asked Questions
What type of cartridge filling machine is best for adhesives?
The best architecture matches the named adhesive, source container, cartridge, closure, released-output target, changeover plan, and inspection method. Choose manual, semi-automatic, or automatic equipment only after those boundaries are fixed.
Can the same machine fill 1K and 2K cartridges?
Only if the supplier proves separate material paths, tooling, recipes, chamber-dose verification, cleaning, and change control for every quoted format. A generic 1K/2K capability statement is not acceptance evidence.
How does a cartridge filling machine reduce trapped air?
It can coordinate bulk condition, material delivery, nozzle position, bottom-up motion, cutoff, and closure insertion. No single feature guarantees an air-free package, so the complete sequence needs product-specific validation.
What information should be included in a machine RFQ?
Include material documents, source containers, package drawings, closures, output cases, changeovers, inspections, utilities, layout, safety requirements, documentation, spares, training, and the FAT protocol.
What should a cartridge filling machine FAT test?
Test startup, normal running, bulk change, format change, planned stop, restart, faults, rejects, closing, marking, inspection, and safe shutdown with agreed materials, packages, methods, records, and acceptance criteria.
Conclusion
Cartridge filling machines should be purchased as controlled production systems, not isolated dosing stations. Freeze the filled package first, map the full line, separate 1K and 2K requirements, and make every performance claim answerable by an agreed test. That sequence protects both procurement and engineering from attractive quotes built on hidden assumptions.
- Define released output as closed, marked, inspected, accepted cartridges.
- Compare identical system boundaries and record every supplier exception.
- Challenge startup, changeover, restart, fault, and reject states during FAT.
- Retain raw evidence, settings, samples, deviations, and the final approved configuration.
The final buying decision should leave a traceable evidence pack: package drawings, material route, machine boundary, exception register, witnessed results, open-item disposition, and release signatures. To review a proposed package and filling-machine interface, contact Haijing’s engineering team with the formulation class, source container, cartridge drawing, closure set, and required output cases.