Introduction: The Core Answer to Medical Device Dispensing
Medical device adhesive dispensing is the controlled, repeatable, micron-precision deposition of biocompatible adhesives onto the bond faces of catheter hubs, needle (cannula-to-hub) joints, and microfluidic chips—creating permanent, leak-free bonds that never intrude into the lumen and meet ISO 10993 / USP Class VI compliance. Success depends on three things: ① the right curing chemistry; ② the right pairing of two-component cartridge + static mixer + precision nozzle; ③ closed-loop volumetric metering in a clean environment that controls shot size to the microliter and avoids bubbles and lumen blockage. Below we break it down by application → material → system → process to help you specify a validatable, production-ready dispensing solution.
Why Medical Bonding Demands Precision Dispensing
Bonded medical parts sit directly in the path of blood, medication, or tissue—any microscopic failure becomes a recall and a compliance risk. Compared with consumer electronics, medical bonding carries four harder constraints:
- Biocompatibility: Adhesives and the packaging system must pass ISO 10993 cytotoxicity / sensitization / irritation screening; fluid-path components often require USP Class VI certification.
- Lumen-safe: The internal bore of catheters and needles must never be infiltrated by adhesive, or the part is scrapped.
- Cleanroom & purity: Particle and extractable control is the baseline, and the package itself must not be a contamination source—this is why silicone-free cartridges are strongly demanded in electronic-grade medical scenarios.
- Pull-strength & seal consistency: Joints must hold position and seal after sterilization cycles; manufacturing typically uses six-sigma control limits.
Authority reference: Henkel’s *Needle Bonding Design Guide* notes that cannula-to-hub joints are geometrically complex and produced in high volume, and that a mismatch between adhesive selection and curing equipment makes the validation cycle “long and expensive”—exactly why the dispensing system should be selected as a complete engineering problem (Henkel Needle Bonding Guide).
Three Core Application Scenarios
1. Catheter Hub Bonding
A catheter is built by inserting multi-lumen tubing into a plastic hub. The dispensing goal is a circumferential ring along the joint that covers the interface with zero gaps, while closed-loop volumetric metering keeps the deposited volume precise—wetting the interface only, never wicking into the lumen by capillary action.
Key points:
- Ring-path accuracy: Use CCD vision to confirm tube-to-hub alignment first, then run the ring path so every part is positioned consistently.
- Volume safety: The capillary creep during cannula insertion should be “just enough to fill the interface,” not “overflow into the bore”—achieved with closed-loop volumetric dosing at the dispensing valve.
- Multi-lumen / side-port geometry: One line must adapt to different joint shapes; the path must be programmable.
2. Needle Bonding (Cannula-to-Hub)
Syringe needles, blood-collection needles, and IV cannulae all bond a stainless-steel cannula into a plastic or glass hub. Here leak prevention (blood / medication) and cannula position fixation are equally critical.
- Curing system: Medical-grade UV-cure acrylic, light-cure cyanoacrylate (requires a light-transmitting material), and single-part heat-cure epoxy are the mainstream candidates.
- Geometry & flow: Joint gaps are small (often <0.1 mm); low-viscosity adhesive wicks in and cures within seconds, while high-viscosity adhesive stays on the surface and does not run before insertion.
- Fluorescent & inspection: Medical-grade formulations often come in a fluorescent version for inline visual QC.
3. Microfluidic Chip Sealing
Microfluidic channels are typically tens to hundreds of microns wide, demanding extreme repeatability and alignment compensation. Customer cases show that a workstation with ±1% repeat positioning plus automatic needle calibration can lift microfluidic chip yield from 95% to 99.8%. This is usually the domain of an automated coordinate dispensing robot.
How to Choose the Right Adhesive Chemistry
| System | Typical viscosity | Cure method | Best for |
|---|---|---|---|
| UV-cure acrylic (medical grade) | 1,000–10,000 mPa·s | UV 365–405 nm, 5–20 s | Fluid-path-compatible catheter hub & needle fast bonding |
| Light-cure cyanoacrylate | 500–5,000 mPa·s | UV 365 nm, 3–10 s | High-volume IV catheter / needle ring fast cure |
| Two-part medical epoxy (2-part medical epoxy) | 2,000–15,000 mPa·s | Room temp or heat cure 40–60°C | High pull-strength structural bonding of multi-lumen / complex hubs |
| Medical silicone | 3,000–20,000 mPa·s | Heat 60–80°C or UV | Flexible parts requiring stress absorption |
Selection rule: If the downstream is electronic-grade / analytical instrumentation and you worry about silicone contamination, prioritize a silicone-free formulation and matching packaging. Our medical-grade silicone-free cartridges and Luer Lock precision needles are injection-molded from medical-grade, USP Class VI-compliant polymers in an ISO-certified clean environment, with full material traceability across the supply chain.
Dispensing Hardware: How to Match Cartridge, Mixer & Nozzle
For a two-part system, the core is not “buy a single cartridge” but matching cartridge + static mixer + gun/nozzle to the material viscosity and mix ratio.
Two-Component Cartridges
Available in mix ratios of 1:1 / 2:1 / 4:1 / 10:1 and sizes such as 25 mL and 50 mL. For medical grade, prefer silicone-free, medical PP dual-component cartridges to avoid extractable contamination.
Static & Dynamic Mixers
Helical / square-element mixers fold and blend the A and B components in flow; more elements mean better mixing but higher back pressure. Selection depends on viscosity difference, mix ratio, and outlet diameter. See our static & dynamic mixer series and the companion methodology *How to Match Dual-Component Cartridges, Static Mixers & Dispensing Guns*.
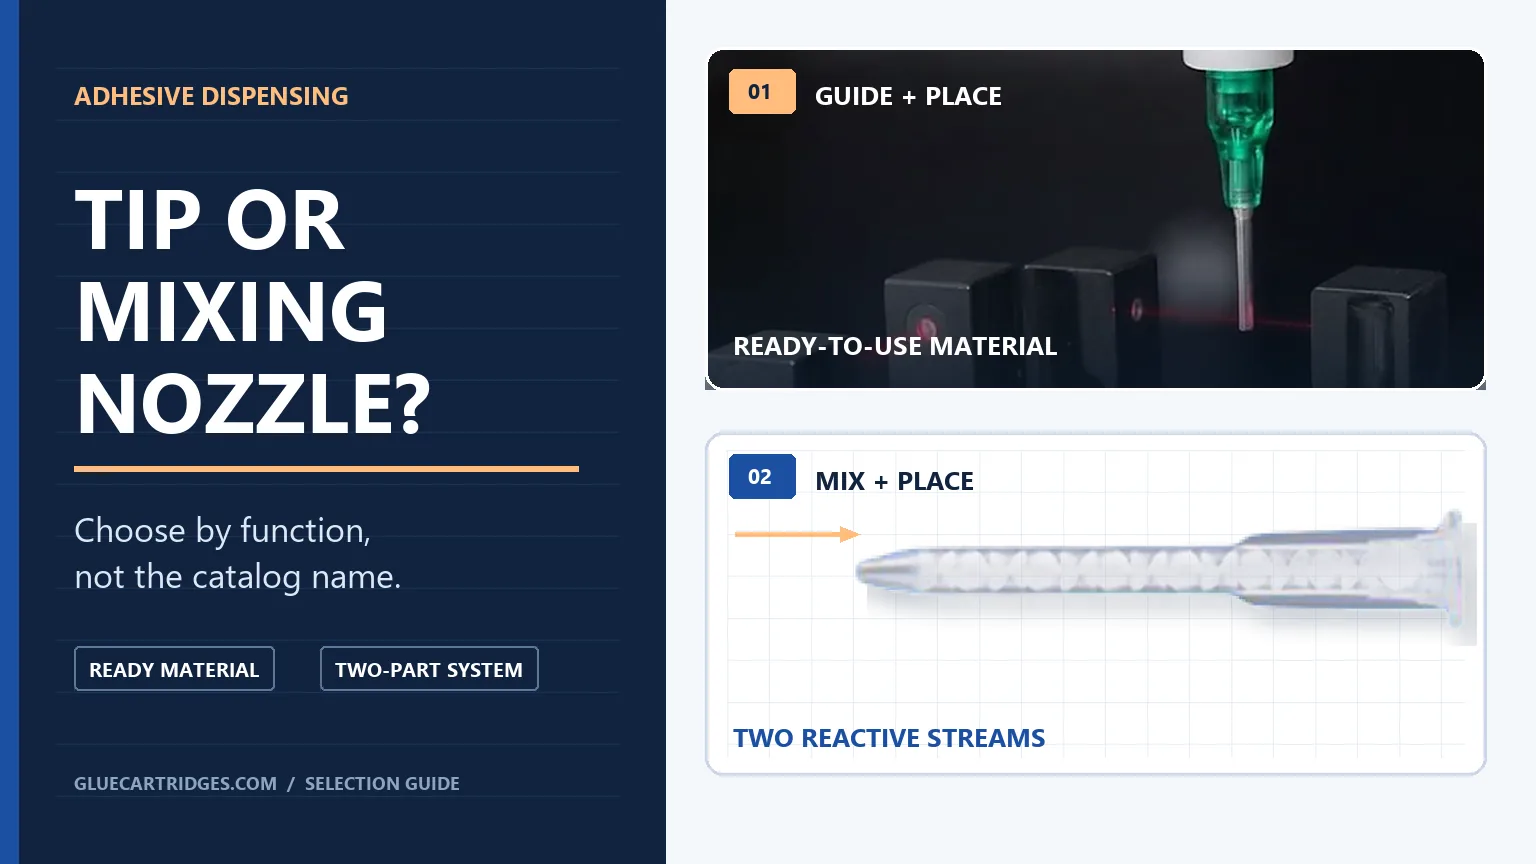
Precision Dispense Tips & Nozzles
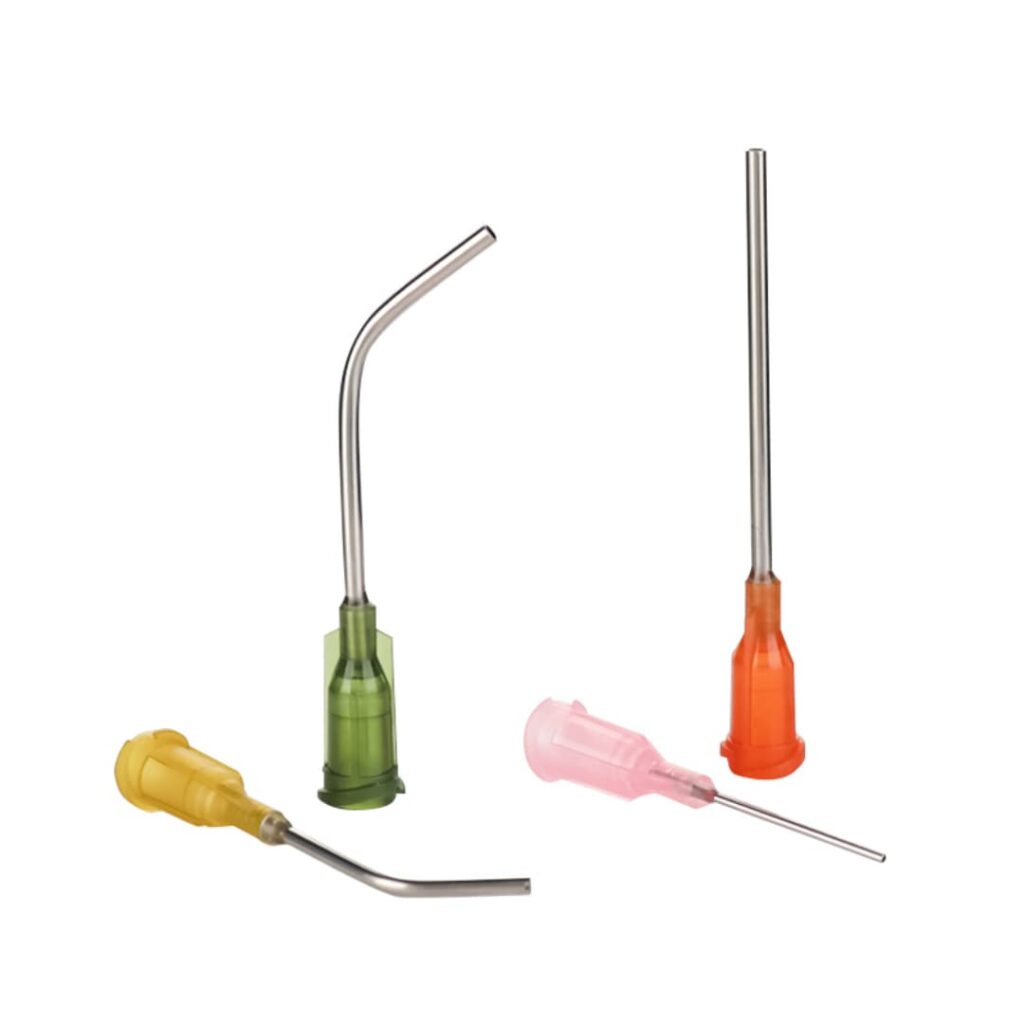
Microliter deposition relies on Luer Lock precision needles and tapered nozzles for repeatable bead diameter and dot placement; medical micro-dispensing commonly uses stainless steel needles with secure locking to avoid dripping and cross-talk.
Industry practice: ProMixUSA emphasizes that disposable static mixers must be “sized to viscosity / mix ratio and purged of 1–2 mixer lengths first,” otherwise the unmixed front material goes straight onto the part as a hidden defect (ProMixUSA).
Manual or Automatic? When to Move to a Dispensing Robot
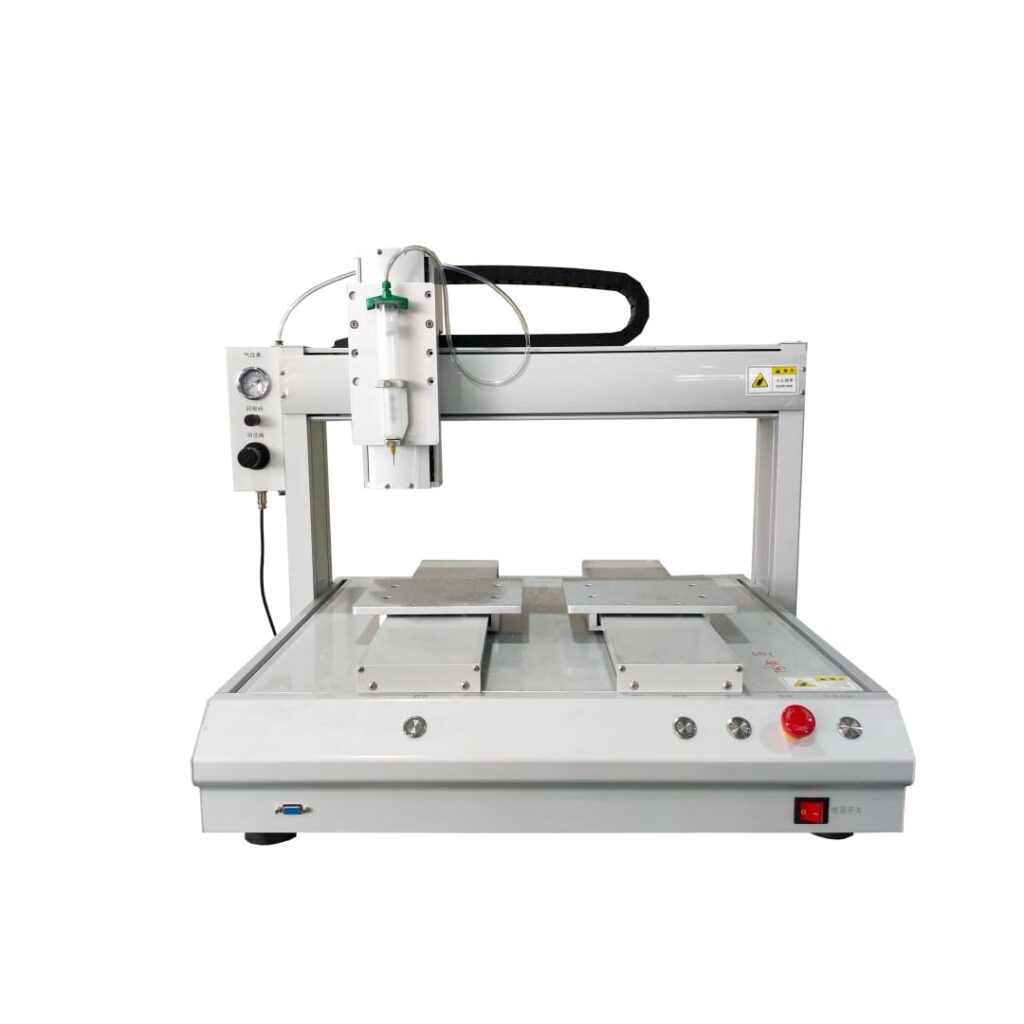
| Dimension | Manual / pneumatic gun | Coordinate applicator (dispensing robot) |
|---|---|---|
| Cycle time | Low–medium | High, ±1% repeat positioning |
| Consistency | Operator-dependent | Programmed, 999 programs stored |
| Typical use | Low volume, repair, R&D prototyping | Catheter / microfluidic million-unit production |
| Alignment | Visual | CCD vision auto-compensation, laser height sensing |
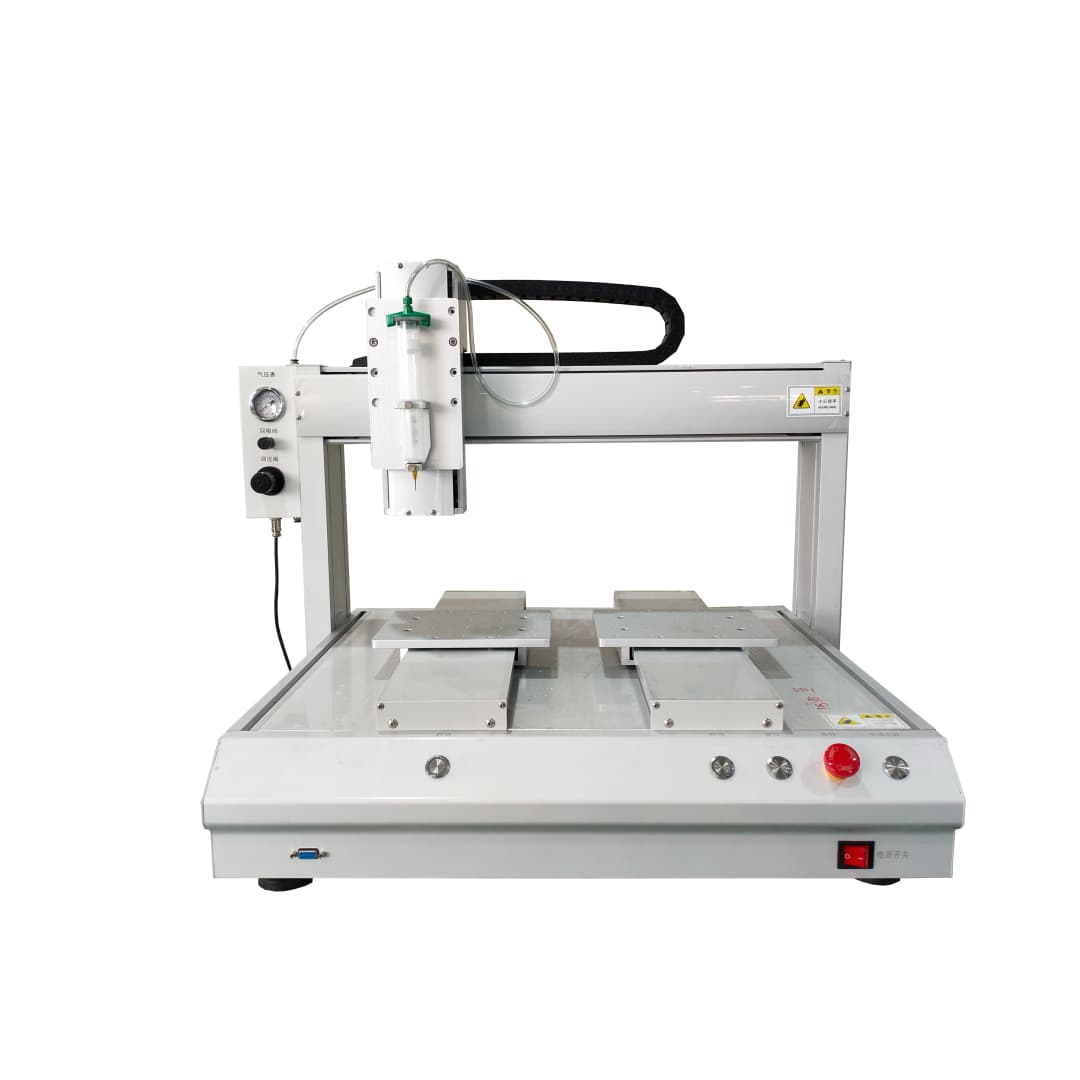
When a product moves to volume production and yield is decided by “consistent every time,” a coordinate dispensing robot is the better choice: it integrates volumetric metering, vision alignment, and path programming into one validatable line. Learn about our Coordinate Applicator automated dispensing workstation.
Process Checklist for Reliable Medical Bonding
- Load & vision align: CCD confirms tube/hub position and joint-face alignment.
- Precision ring / dot dispense: Closed-loop volumetric metering wets the interface only, never intruding into the lumen.
- Assemble in place: Cannula inserts to target depth; adhesive wets the interface.
- Cure: UV or heat cure per formulation to form a permanent, leak-free joint.
- Validate: Spot-check pull strength and pressure leak test to confirm joint integrity.
- Environment: Store and handle adhesive and packaging in a clean, temperature-controlled, UV-avoided environment; refrigerated material must return to room temperature before use.
Common Defects & How to Avoid Them
- Air bubbles: From incomplete cartridge degassing or poor mixing; purge first, use low-back-pressure mixers, vacuum-degas if needed.
- Lumen intrusion: Excess volume or uncontrolled capillary action; constrain with closed-loop volumetric dosing and programmed paths.
- Off-ratio: Piston wear, seal leakage, mixer mismatch; perform periodic A/B weigh verification and mixer-matching checks.
- Incomplete cure: Wrong light intensity / wavelength or thermal profile; verify the cure window against the TDS.
FAQ
Q1: What is the biggest difference between medical device adhesive dispensing and industrial dispensing? A: It comes down to compliance and purity—ISO 10993 / USP Class VI-grade materials, a clean environment, zero lumen intrusion, and a process that is validatable and traceable, not just fast.
Q2: How do you prevent adhesive from entering the catheter lumen? A: Use closed-loop volumetric metering so the adhesive wets the joint interface only, combined with CCD vision alignment and a programmable ring path; the capillary creep during cannula insertion must be calibrated against real parts.
Q3: Does two-part medical epoxy always require a static mixer? A: Yes. A two-part system relies on the static mixer to homogenize A/B in flow; wrong element count or mismatched interface causes off-ratio and incomplete cure. See the matching guide.
Q4: Why does medical scenarios emphasize silicone-free cartridges? A: Silicone extractables contaminate electronic-grade / analytical medical channels; silicone-free medical PP cartridges + Luer Lock needles avoid this contamination and meet purity requirements.
Q5: What equipment for low-volume prototyping, and what for volume production? A: Prototyping can use a manual / pneumatic gun; once you reach million-unit production where yield is set by consistency, upgrade to a coordinate dispensing robot (±1% repeat positioning + vision compensation) for better economics.
Conclusion & Action Plan
Medical device dispensing is not “buy a glue gun”—it is specifying a system engineering of biocompatible material + silicone-free compliant packaging + matched mixer/nozzle + validatable automation line. First lock the application (catheter / needle / microfluidic) and the curing chemistry, then match medical-grade silicone-free cartridges and needles, static mixers, and a coordinate dispensing robot, and finally use the process checklist to lock yield into the line.
Need a custom dispensing solution for your catheter / needle / microfluidic product? Our engineering team provides one-stop OEM/ODM customization from tooling development and material selection to high-precision molding, typically returning a professional proposal and quote within one business day. You can also read the cluster-mate Automotive Electronics Adhesive Dispensing Guide to understand cross-industry selection logic.